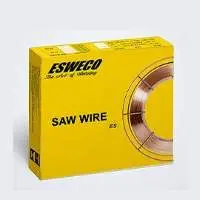
ES EL12 is a copper-coated, mild steel wire for submerged arc welding.
It can be combined with the following fluxes:
ES FLUX 171, ES FLUX 180
ES FLUX 181 and ES FLUX 900.
ES EL12 is especially for use in combination with ES FLUX 180 and ES FLUX 181 in the shipbuilding industry, for the butt welding in material from 10 to 30 mm thickness and especially thin plate (e.g. LPG cylinder).
ES FLUX 900 is a basic agglomerated, slightly Si- and Mn-alloying fux for submerged arc welding, specially designed for fillet welding and for the single- and multi-pass butt welding of mild, medium and high tensile steels.
ES FLUX 900 is of the aluminate basic type and, for this slag system, it has a very high current-carrying capacity on both AC and DC and very good operating characteristics.
ES FLUX 900 is ideally suited to narrow gap welding due to the excellent slag detachability and smooth side-wall blending.
ES FLUX 171 is a basic agglomerated, slightly Si- and Mn-alloying fux for submerged arc welding, specially designed for fillet welding and for the single- and multi-pass butt welding of mild, medium and high tensile steels.
ES FLUX 171 is of the aluminate basic type and, for this slag sys- tem, it has a very high current-carrying capacity on both AC and DC and very good operating characteristics.
ES FLUX 171 is ideally suited to narrow gap welding due to the excellent slag detachability and smooth side-wall blending.
ES FLUX 161 is designed for the single-wire, multi-run butt welding of mild, medium and high tensile steels with impact strength requirements down to -40C/-60C.
Due to the non-alloying effect, ES FLUX 161 is designed for use with a suitable alloying wire. ES FLUX 161 can be used on DC.
ES FLUX 900 is a basic agglomerated, slightly Si- and Mn-alloying fux for submerged arc welding, specially designed for fillet welding and for the single-and multi-pass butt welding of mild, medium and high tensile steels. ES FLUX 900 is of the aluminate basic type and, for this slag system, it has a very high current-carrying capacity on both AC and DC and very good operating characteristics.
ES FLUX 900 is ideally suited to narrow gap welding due to the excellent slag detachability and smooth side-wall blending.
Density
2487 Welding Wires Supplies Suppliers
Short on time? Let Welding Wires Supplies sellers contact you.
ES FLUX 180 is designed for use in the single-and multi-pass butt welding of mild and medium tensile steels where moderate impact strength is required.
ES FLUX 180 is of the calcium-silicate type with a very high current-carrying capacity, even at low welding speeds with both AC and DC.
ES FLUX 180 is excellent for the butt welding of materials from 10 to 30 mm thickness and is used in the shipbuilding industry, for example.
ES FLUX 180 is specially designed for use in combination with ES EL12 or ES EM12 in single- or multi-wire systems.
ES FLUX 171 is a basic agglomerated, slightly Si- and Mn-alloying fux for submerged arc welding, specially designed for fillet welding and for the single and multi-pass butt welding of mild, medium and high tensile steels. ES FLUX 171 is of the aluminate basic type and, for this slag system,
It has a very high current-carrying capacity on both AC and DC and very good operating characteristics.
ES FLUX 171 is ideally suited to narrow gap welding due to the excellent slag detachability and smooth side-wall blending.
ES EA4 is a manganese-alloyed, copper coa-ted wire for the submerged arc welding of medium- and high-strength structural steels.
ES EA4 should preferably be used together with non-alloying or slightly alloying fuxes, such as ES FLUX 161, when high weld metal quality requirements must be met.
ES EA4 Submerged arc welding wire (SAW) for joining fine grain and high temperature resistant steels, structural steels, steels for shipbuilding, steels for pressure vessels, production of steel pipes up to grade X80, high-strength steels, etc.
ES EA4 can be combined with ES FLUX 161, ES FLUX 171 and ES FLUX 900.
ES EA2 is a copper-coated, molybdenum-alloyed wire for the submerged arc welding of non-alloyed and low-alloyed steels.
ES EA2 Submerged arc welding wire (SAW) used for joining fine grain steels resistant to high temperatures, structural steels, construction naval vessels, pressure vessels, shipbuilding steels, pipes and pipeline steels up to grade X70, etc.
ES EA2 can be combined with ES FLUX 161, ES FLUX 171 and ES FLUX 181.
ES EM12 is a copper-coated, semi-killed wire for the submerged arc and electro-slag wel ding of medium and high strength structural steels.
It can be combined with the following fluxes:
ES FLUX 171, ES FLUX 180
ES FLUX 181 and ES FLUX 900.
ES EM12 can be applied both for high-speed welding steel plate of 450-500 MPa tensile stren-gth steel (e.g. boiler, bridge, pressure vessel, and LPG cylinder).
ES FC 316LT is a fux-cored wire for the out-of-position welding of 316 and 316L type stainless steels where increased resistance to pitting corrosion is required.
This is particularly relevant when it comes to attack by chloride solutions and sulphuric acid.
The weld metal composition is such that the stabilised 321 and 347 stainless steels may also be welded.
ES FC 308LT is a rutile, fux-cored wire, speci�cally designed to operate in the vertical and overhead positions when welding 304, 304L, 308 and 308L stainless steels.
The stabilised 321 and 347 steels may also be welded.
Typical application: welding 304L and other common 18/8 stainless steels, Nitrogen bearing 304LN and titanium stabilized 321 and General fabrication including piping, tanks, and pressure vessels
ES 81T1-Ni1M is an all-positional, rutile, fux- cored wire for good toughness down to -40C.
The wire contains 1% nickel and has exceptional operating characteristics in all positions with high deposition rates. Shielding gas Ar + 20% CO2 or CO2. ES 81T1-Ni1M is designed for the all-posit-ional welding of carbon-manganese and low-alloy steels.
Typical applications: offshore fabrications, vessels and structural steel work.
ES 71T1M is a fux-cored, tubular wire designed as a truly all-positional, general-purpose wire for welding mild and medium tensile steels up to 510 MPa tensile strength.
Using either Ar/CO2 or CO2 as the shielding gas, the 1.2 and 1.4 mm sizes can be used in the vertical position on spray transfer providing for maximum deposition and time savings.
Weld pool control is easy both vertically up and downwards and slag removal is rapid. ES 71T1M is designed for a wide range of applications especially where manipulation of the work is impractical.
ES 71T1M is a Fux-cored, tubular wire designed as a truly all-positional, general-pur pose wire for welding mild and medium tensile steels up to 510 MPa tensile strength.
Using either Ar/CO2 or CO2 as the shielding gas, the 1.2 and 1.4 mm sizes can be used in the vertical position on spray transfer providing for maximum deposition and time savings.
Weld pool control is easy both vertically up and downwards and slag removal is rapid.
ES 71T1M is designed for a wide range of applications especially where manipulation of the work is impractical.
ES MIG 5356 is the most widely used welding alloy and can be classified as a general-purpose type filler alloy.
ES MIG 5356 is typically cho- sen because of its relatively high shear strength.
The 5XXX alloy base material, welded with ES MIG 5356, with a weld pool chemistry greater than 3% Mg and service temperatures in excess of 65�°C, is susceptible to stress corrosion cracking.
ES MIG 5183 is designed to provide the highest possible strength in the as-welded condition of alloy AA 5083 and similar high-magnesium alloys.
The more common ES MIG 5356 typi- cally fails to meet the as-welded tensile require- ments of AA 5083.
The alloy is typically used in marine and structural applications where high strength, high fracture toughness for impact resistance and exposure to corrosive elements are important.
The alloy is not recommended for elevated temperature applications due to its susceptibility to stress corrosion cracking. The alloy is non-heat treatable.
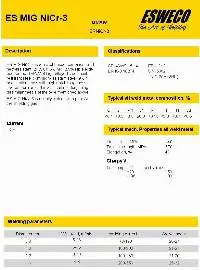
ES MIG NiCr-3 is a nickel-based, corrosion and heat-resistant, 20% Cr, 3% Mo, 2.5% Nb electr-ode for the GMAW of high-alloyed steel, heat-resistant steel, corrosion-resistant steel, 9% Ni and similar steels with high notch toughness at low temperatures.
It is also suitable for joining dissimilar metals of the type mentioned above.
ES MIG NiCr-3 is usually welded with pure Ar as the shielding gas.
ES MIG 2209 a continuous, solid, corrosion-resistant, duplex wire for welding austenitic-ferritic stainless alloys of the 22% Cr, 5% Ni, 3% Mo types.
ES MIG 2209 has high general corrosion resistance. In media containing chloride and hydrogen sulphide, the alloy has a high resis- tance to intergranular corrosion, pitting and espe- cially to stress corrosion.
The alloy is used in a variety of applications across all industrial seg- ments.
ES MIG 316LSi a continuous, solid , corrosion-resistant, chromium-nickel-molybdenum wire for welding austenitic stainless alloys of the 18% Cr -8% Ni and 18% Cr -10% Ni -3% Mo types.
ES MIG 316LSi has good general corrosion resistance; in particular, the alloy has very good resistance to corrosion in acid and chlorinated environments.
The alloy has a low carbon con- tent which makes it particularly recommended when there is a risk of intergranular corrosion.
The higher silicon content improves the welding properties such as wetting.
The alloy is widely used in the chemical and food processing industries, as well as in shipbuilding and various types of architectural structure.
ES MIG 312 a continuous, solid, corrosion-resistant, chromium-nickel wire for welding stainless steels of the 29% Cr, 9% Ni types.
ES MIG 312 has good oxidation resistance at high temperatures due to its high content of Cr.
The alloy is widely used for joining dissimilar steels, especially if one of the components is fully austenitic, and steels that are difucult to weld, i.e. machine components, tools and austenitic-manganese steels.
ES MIG 309LSi a continuous, solid ,corrosion-resistant, chromium-nickel wire for welding steels with a similar composition, wrought and cast steels of the 23% Cr -12% Ni types.
The alloy is also used for welding buffer layers on C/Mn steels and welding dis similar joints.
When using the wire for buffer layers and dissimilar joints, it is necessary to control the dilution of the weld.
ES MIG 309LSi has good general corrosion resistance.
The higher silicon content improves the welding properties such as wetting.
ES MIG 309LSi a continuous, solid ,corrosion-resistant, chromium-nickel wire for welding steels with a similar composition, wrought and cast steels of the 23% Cr -12% Ni types.
The alloy is also used for welding buffer layers on C/Mn steels and welding dis similar joints.
When using the wire for buffer layers and dissimilar joints, it is necessary to control the dilution of the weld.
ES MIG 309LSi has good general corrosion resistance.
The higher silicon content improves the welding properties such as wetting.
ES MIG 80S-Ni1 is a 0.9Ni-alloyed (ER80S-Ni1), copper-coated, solid wire for the GMAW of low-temperature, ne-grained steels.
The wire provides good impact toughness down to -50C and is especially suitable for use in the construction of offshore platforms, pressure vessels, and pipelines.
ES MIG 80S-G is a 0.5Mo-alloyed, solid wire for the GMAW of creep-resistant steels of the same composition, like those used for pipes in press-ure vessels and boilers with a service tempera-ture of up to 500�°C.
ES MIG 80S-G is taking MAG welding operations to new levels of performance and all-round ef�ciency, especially in robotic and mechanised welding.
Characteristic features include excellent start properties; trou- ble-free feeding at high wire speeds and lengthy feed distances; a very stable arc at high welding currents; extremely low levels of spatter; low fume emission; reduced contact tip wear and improved protection against corrosion of the wire.
ES MIG 70S-3 is a copper-coated, Mn-Si-allo-yed G2Si/ER70S-3 solid wire for the GMAW of non-alloyed steels, as used in general construction, pressure vessel fabrication and shipbuil-ding.
The wire has a carefully controlled wire chemistry and a unique surface technology providing superior weld-metal quality at high wire feed speeds and at high welding currents.
The wire can be used with both Ar/CO2 mixed gas and pure CO2 shielding gas.
ES TIG 5356 is the most widely used welding alloy and can be classified as a general-purpose type �ller alloy.
ES TIG 5356 is typically chosen because of its relatively high shear strength.
The 5XXX alloy base material, welded with ES TIG- 5356, with a weld pool chemistry greater than 3% Mg and service temperatures in excess of 65C, is susceptible to stress corrosion crack- ing.
A nickel-based rod alloyed with about 30% Cu, 2% Ti and 1% Fe for the GTAW of base materials of the same type. It can also be used for joining these alloys to steels.
ES TIG NiCu-7 is norm-ally welded with pure Ar as the shielding gas.
Typical applications include heat exchangers, piping, pumps, valves and process vessels in the chemical, offshore and marine industries.
A nickel-based, corrosion- and heat-resistant, 22% Cr, 9% Mo, 3.5% Nb rod for the GTAW of high-alloyed steel, heat-resistant steel, corrosion-resistant steel, 9% Ni steels and similar steel with high notch toughness at low tempera- tures.
It is also suitable for joining dissimilar metals of the types mentioned above.
ES TIG NiCrMo-3 is normally welded with pure Ar as the shielding gas.
A nickel-based, corrosion- and heat-resistant, 20% Cr, 3% Mn, 2.5% Nb rod for the GTAW of high-alloyed steel, heat-resistant steel, corro-sion-resistant steel, 9% Ni steels and similar steels with high notch toughness at low temperatures.
It is also suitable for joining dissimilar metals of the types mentioned above.
ES TIG NiCr-3 is usually welded with pure Ar as the shielding gas.
Bare, corrosion-resistant, duplex welding rods for welding austenitic-ferritic stainless alloys of the 22% Cr, 5% Ni, 3% Mo types.
ES TIG 2209 has high general corrosion resistance. In media containing chloride and hydro- gen sulphide, the alloy has high resistance to intergranular corrosion, pitting and especially to stress corrosion. The alloy is used in a variety of applications across all industrial segments.
Bare, corrosion-resistant, chromium-nickel rods for welding stabilised austenitic chromium-nickel alloys of the 18% Cr-8% Ni type.
The rods are stabilised with niobium, which provides good resistance to the intergranular corro- sion of the weld metal. Due to the niobium content, this alloy is recommended for use at hig- her temperatures.
Bare, corrosion-resistant, chromium-nickel welding rods for welding materials of the 29% Cr, 9% Ni types.
ES TIG 312 has good oxidation resistance at high temperatures due to its high content of Cr.
The alloy is widely used for joining dissimilar steels, especially if one of the components is fully austenitc, and for steels that are dificult to weld, i.e. machine components, tools and austenitic-manganese steels.
Bare, corrosion-resistant, chromium-nickel welding rod for welding the 24%Cr, 13%Ni alloyed types of steel.
The alloy is also used for welding buffer layers on C/Mn steels and for welding dissi- milar joints. When using the wire for buffer layers and dissimilar joints, it is necessary to control the dilution of the weld.
ES TIG 309L has good general corrosion resistance.
When used for joining dissimilar materials, the corrosion resistance is of secon- dary importance.
Bare, corrosion-resistant, chromium-nickel TIG rod. ES TIG 308L has good general corrosion resistance.
The alloy has a low carbon content which makes it particularly recommended when there is a risk of intergranular corrosion.
The alloy is widely used in the chemical and food-processing industries, as well as for pipes, tubes and boilers. Suitable for the joining of stainless steels of the18% Cr-8% Ni type with a low carbon content and Nb-stabilised steels of the same type if the service temperature does not exceed 350C.
It can also be used for welding Cr steels, except in sulphur-rich environments.
ES TIG 90S-B3 is a 2.5Cr-1.1Mo-alloyed (ER90S-B3), copper-coated rod for the GTAW of creep-resistant steels like SA-387 Grade 22, A335 Grade P22 or similar materials.
ES TIG 90S-B3 typically used in chemical industries for heat exchangers, boilers, piping and pressure vessels at service temperatures up to 1100F (590 C)
ES TIG 80S-Ni2 is 2.4Ni-alloyed (ER80S-Ni2), copper-coated rod for the GTAW of low-temperature, �ne-grained steels in applications such as pressure vessels, pipes and the offshore indus- try, with a minimum yield strength of up to 470 MPa. The wire provides good impact toughness down to -60C.
2487 Welding Wires Supplies Suppliers
Short on time? Let Welding Wires Supplies sellers contact you.