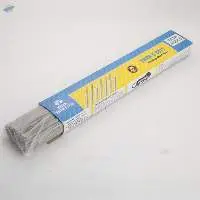
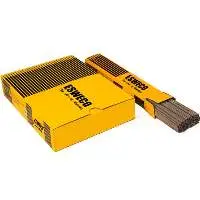
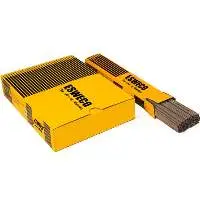
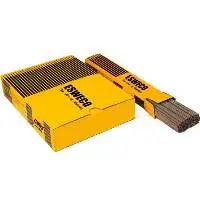
Achieve superior welding results with the Tata Agrico Mild Steel Electrode ISI Grade Radiographic Quality, engineered for exceptional performance and reliability, making it the ideal choice for critical applications where a radiographic quality weld deposit is required.
Technical Specification:
Material Description 2.70 X 450 mm
Quantity Quantity in Master Box: 12 Packets
Standard Packaging 90
Achieve superior welding results with the Tata Agrico Mild Steel Electrode ISI Grade Radiographic Quality, engineered for exceptional performance and reliability, making it the ideal choice for critical applications where a radiographic quality weld deposit is required.
Technical Specification:
Material Description 2.70 X 350MM
Quantity Quantity in Master Box: 12 Packets
Standard Packaging 90
Achieve superior welding results with the Tata Agrico Mild Steel Electrode ISI Grade Radiographic Quality, engineered for exceptional performance and reliability, making it the ideal choice for critical applications where radiographic quality weld deposit is required.
Technical Specification:
Material Description 3.70 X 450 mm
Quantity Quantity in Master Box: 12 Packets
Standard Packaging 60
Achieve superior welding results with the Tata Agrico Mild Steel Electrode ISI Grade Radiographic Quality, engineered for exceptional performance and reliability, making it the ideal choice for critical applications where a radiographic quality weld deposit is required.
Technical Specification:
Material Description 2.90 X 350 mm
Quantity Quantity in Master Box: 12 Packets
Standard Packaging 90
Get clean, strong, and rust-resistant welds with the Tata Agrico Stainless Steel Electrode, designed for stainless steel jobs where durability, corrosion resistance, and a polished finish matter, perfect for kitchens, fabrication, and industrial use.
Technical Specification:
Material Description 4.00 X 350 mm
Quantity Quantity in Master Box: 5 Packets
Standard Packaging 38
1593 Electrodes Suppliers
Short on time? Let Electrodes sellers contact you.
Ideal for everyday welding needs, the Tata Agrico Mild Steel Electrode ISI (E6013) offers smooth arc stability and clean & Rippled Curve weld finishes, making it perfect for general-purpose fabrication, light structures, and repair work.
Technical Specification:
Material Description 4.00 X 450
Quantity Quantity in Master Box: 8 Packets
Standard Packaging 55
Ideal for everyday welding needs, the Tata Agrico Mild Steel Electrode ISI (E6013) offers smooth arc stability and clean & Rippled Curve weld finishes, making it perfect for general-purpose fabrication, light structures, and repair work.
Technical Specification:
Material Description 4.00 X 450 mm
Quantity Quantity in Master Box: 12 Packets
Standard Packaging 55
Ideal for everyday welding needs, the Tata Agrico Mild Steel Electrode ISI (E6013) offers smooth arc stability and clean & Rippled Curve weld finishes, making it perfect for general-purpose fabrication, light structures, and repair work.
Technical Specification:
Type Tata E6013 Bluebond
Material Description 3.15 X 450 mm
Quantity Quantity in Master Box: 6 Packets
Standard Packaging 90
Ideal for everyday welding needs, the Tata Agrico Mild Steel Electrode ISI (E6013) offers smooth arc stability and clean & Rippled Curve weld finishes, making it perfect for general-purpose fabrication, light structures, and repair work.
Technical Specification:
Type Tata â?? E6013 Bluebond
Material Description 2.50 X 350 mm
Quantity Quantity in Master Box: 12 Packets
Standard Packaging 100
Ideal for everyday welding needs, the Tata Agrico Mild Steel Electrode ISI (E6013) offers smooth arc stability and clean & Rippled Curve weld finishes, making it perfect for general-purpose fabrication, light structures, and repair work.
Technical Specification:
Material Description 3.15 X 350 mm
Quantity Quantity in Master Box: 12 Packets
Standard Packaging 85
Ideal for everyday welding needs, the Tata Agrico Mild Steel Electrode ISI (E6013) offers smooth arc stability and clean & Rippled Curve weld finishes, making it perfect for general-purpose fabrication, light structures, and repair work.
Technical Specification:
Material Description 3.15 X 450 mm
Quantity Quantity in Master Box: 8 Packets
Standard Packaging 90
Ideal for everyday welding needs, the Tata Agrico Mild Steel Electrode ISI (E6013) offers smooth arc stability and clean & Rippled Curve weld finishes, making it perfect for general-purpose fabrication, light structures, and repair work.
Technical Specification:
Material Description 3.15 X 350 mm
Quantity Quantity in Master Box: 8 Packets
Standard Packaging 90
Ideal for everyday welding needs, the Tata Agrico Mild Steel Electrode ISI (E6013) offers smooth arc stability and clean & Rippled Curve weld finishes, making it perfect for general-purpose fabrication, light structures, and repair work.
Technical Specification:
Material Description 5.00 X 450 mm
Quantity Quantity in Master Box: 12 Packets
Standard Packaging 40
(1) Regular power graphite electrode( RP grade Graphite Electrode) . Graphite electrode with current density less than 17a / cm2 is allowed to be used in common power electric furnaces for steelmaking, silicon smelting and yellow phosphorus smelting.
(2) Oxidation resistant coating graphite electrode. A graphite electrode coated with an anti-oxidation protective layer (graphite electrode anti oxidant). The formation of both conductive and high temperature oxidation resistant protective layer can reduce the electrode consumption (19% ~ 50%), prolong the service life of the electrode (22% ~ 60%), and reduce the electric energy consumption of the electrode. The popularization and application of this technology can bring such economic and social effects as follows: 1. The unit consumption of graphite electrode is less, and the production cost is reduced to a certain extent. For example, according to the consumption of 35 graphite electrodes per week and 165 refining heats of LF refining furnace in a steel-making plant without shutdown in the whole year, 373 (153 tons) electrodes can be saved every year by using graphite electrode oxidation resistance technology, and RMB 2585700 can be saved by RMB 16900 per ton of ultra-high power electrode per year. 2 The graphite electrode consumes less electricity, saves the unit electricity consumption of steelmaking, saves the production cost, saves energy! 3. Because the graphite electrode is replaced less times, the labor amount and risk coefficient of operators are reduced, and the production efficiency is improved. 4 Graphite electrode is a high consumption and high pollution product, which has a very important social significance in the days of promoting energy conservation, emission reduction and environmental protection. This technology is still in the stage of research and development in China, and some domestic manufacturers have begun to produce it. It is widely used in Japan and other developed countries. At present, there are also companies that import the anti-oxidation protective coating in China.
(3) High power graphite electrode (HP grade Graphite Electrode). Graphite electrode with current density of 18-25a / cm2 is allowed to be used in high power electric arc furnace for steelmaking.
(4) Ultra high power graphite electrode( UHP grade Graphite Electrode). Graphite electrode with current density greater than 25A / cm2 is allowed. It is mainly used in ultra high power EAF.
POME is always regarded as a highly polluting wastewater generated from palm oil mills. This effluent could be used for biogas production through anaerobic digestion.
Graphite electrodes carry the electric current to create an arc that generates the heat required to melt and/or process various materials in electric arc furnaces (EAF)
used in steel, cement and glass manufacturing, expanded graphite - based sealing gaskets, graphite grease, braid, brushes, brake lining, etc
For price, specifications and other details please contact us
ES EST is a non-nickel, non machinable cast iron electrode.
It is the most economical way to go for repairing various kinds of cast iron products providing that machinability of the weld deposit is not required and where weld shrinkage stress is not a concern.
EST melts at relatively low temperatures which permit the use of low welding currents.
This electrode may be used in any position, utilizing AC or DC (reverse polarity).
A nickel-cored electrode for welding normal grades of cast iron.
The weld metal is soft and easily machinable. Deposition is performed on cold or slightly preheated material.
The electrode is suitable for joining cast iron for the recti�cation of casting and the repair of broken parts.
ES Ni-Cl is specifically suited for repairing cracked or porous castings and to weld cast iron to itself or dissimilar metals such as low alloy and carbon steels.
ES 312-17 is a high-alloyed electrode which deposits a ferritic-austenitic duplex weld metal with approx. 40% ferrite.
It is resistant to stress corrosion and is highly insensitive to dilution.
Good scaling resistance up to 1150�°C. ES 312-17 is used for joining dissimilar steels, steels with reduced weldability and buffer layers prior to hardfacing.
Applications: rolls, forging dies, hot work tools, dies for plastics and so on.
ES 309L-17 is an over-alloyed, stainless electrode for welding stainless to mild steel and low-alloy steel, for surfacing mild steel and for welding the root runs in clad steel.
The electrode has excellent weldability in all positions except vertical down, on both AC and DC.
ES 309L-15 is a basic coated, stainless electrode for welding steels of the 24Cr13Ni type, for welding transition layers when surfacing mild steel with stainless, for joining dissimilar steels and welding root runs in the stainless side of clad steels.
ES 307-25 is a synthetic, high-recovery electrode of the 18Cr8Ni6Mn type for welding dissimilar steels, 13Mn steels, steels with reduced weld-ability and for cladding carbon steels.
ES 310-15 is a stainless-steel electrode for welding 25Cr20Ni steels.
It is also suitable for wel- ding armour steel, austenitic-manganese steel and for joining dissimilar steels.
ES 310-15 depo- sits a very crack-resistant weld metal.
ES 310-15 used for cladding side of stainless clad steels and dissimilar steels, hydrogenation and polymerization plant, gas turbine combustion chamber parts, annealing boxes, high temperature furnace parts up to 1200 C.
ES 308H-15 is a basic coated, stainless-steel electrode of the 308H type.
The electrode is designed for high-temperature applications in petrochemical and chemical process plants.
ES 308H-15 is widely used in petrochemical and chemical process plant, particularly for the fabrication of cyclones, transfer lines operating in the range 400-815C.
Rutile coated electrode for welding 19Cr10Ni type steels.
Also suitable for welding stabilised steels of similar composition, except when the full creep resistance of the base material is to be met.
The electrode is specially designed for wel- ding thin-walled pipes.
ES308L-16 characteristics make this electrode the smart choice for general structural welding, as well as for food, and pharmaceutical equipment applications.
ES 12018-M is recommended for use in fabrication low alloyed high tensile strength steels where weld of 120 ksi (830 MPa) minimum tensile strength are required.
ES 12018-M typically used to weld forging, casting plate and pressure vessels, automotive industrial and general fabrication, mobile equipment's railcars.
ES 10018-M used for welding high strength low alloy steels in the 100,000 psi tensile strength range.
It is ideal for conditions of high heat and humidity due to the moisture resistant coating which helps prevent hydrogen cracking and starting porosity.
ES 10018-M is an excellent choice for reinforcing steels and high tensile steels.
Basic low-hydrogen electrode for the AC/DC welding of creep-resistant steels of the 2.3% Cr/1% Mo type, such as SA - 387 Grade 22/A 335 Grade P22 or similar.
The weld metal has the extra-low impurity levels speci�ed in step-cooling requirements.
All-positional, low-hydrogen electrode for welding higher strength steels such as HY-80, HY-90 and ASTM A514, A508, A533, depositing weld metal with a minimum yield strength of 550 N/mm2 after stress relieving.
Typical application such as crane, heavy trans-port, platforms, vessel and lifting equipment in offshore, pipeline.
ES 8018-B8 is an LMA basic electrode contain-ning 9Cr1Mo for the welding of creep-resistant steels.
It is especially suitable for pipe welding.
The electrode runs with a quiet, stable arc and gives a minimum amount of spatter. A prehe-ating and interpass temperature of 150-260�°C is normally required.
The mechanical properties stated here are after one hour of heat treatment at 740C.
ES 8018-B2L is an outstanding welding electrode for higher strength steels with tensile strengths greater than 80,000 psi.
The coating is specially formulated to resist moisture pick-up under cond-itions of high heat and humidity.
The electrode offers resistance to moisture reabsorption, which helps prevent hydrogen cracking and aids in eliminating starting porosity.
ES 8018-B2L is an excellent choice for boiler fabrication and maintenance of pressure piping such as found in steam power generating equip-ment, petrochemical pressure vessels, and che-mical processing equipment and also in the shipbuilding industries.
Basic, low-hydrogen electrode for the DC welding of creep-resistant steels of the 1.25% Cr, 0.5% Mo type, such as SA-387 Grade 11/A 335 P11.The weld metal has an extra-low impurity level.
High tensile, low hydrogen, iron powder electrode for welding 1% Nickel Steels subjected to low temperature service applications especially where notch toughness is required to temperature as low as -60C.
Typical application for ES 8018-C3 is an excel-ent choice for shipbuilding, piping, gas storage tanks, commercial, and military applications.
1593 Electrodes Suppliers
Short on time? Let Electrodes sellers contact you.