Please click here to check who's online and chat with them.

Find Verified Food Chemicals Suppliers, Manufacturers and Wholesalers

GOLD PLUS Member
VERIFIED
Aug-15-26
Supplier From Vadodara, Gujarat, India
 Inquire Now  
Pure, free-flowing unrefined jaggery powder made from concentrated sugarcane juice. Soluble, nutrient-rich healthier alternative to refined white sugar for beverages, baking, and cooking.

Key Advantages
Free-flowing granular texture that dissolves instantly
Zero refined chemicals, bleaching agents, or sulfur dioxide
Natural healthy substitute for white sugar in daily beverages and foods
Sourced directly from vetted sugarcane processing facilities


Technical Specifications
Origin India
Form Fine Granular Powder
Color Golden Yellow / Light Amber
Sucrose Content 72% to 80%
Moisture Max 4.0%
Solubility 100% Water Soluble

Packaging Configurations
500g / 1kg zip-lock stand-up retail pouches
25 kg multi-wall PP bags with inner food-grade liner
Custom private branding options
GOLD PLUS Member
Feb-09-26

Premium Hulled White Sesame Seeds, Grade A

$100 - $1.20K / Metric Ton (CIF)
MOQ: 27  
Sample Available
Supplier From Boulder, Colorado, United States
 Inquire Now  
Our Premium Hulled White Sesame Seeds are 100 natural glutenfree and rich in protein making them an excellent addition to a healthy diet Carefully sourced and processed these sesame seeds deliver exceptional quality flavor and nutritional value for use in baking tahini production snacks salads sauces and health foods

With a high protein and healthy oil content these seeds are ideal for manufacturers wholesalers and retailers seeking cleanlabel agricultural products Our hulled sesame seeds feature a smooth texture mild nutty flavor and are available in bulk quantities with custom packaging and OEM options

Key Features
100 Natural GlutenFree Safe for Sensitive Diets
High Protein Content Great for Health Food Formulations
Smooth Texture Mild Flavor Ideal for Baking Sauces
NonGMO Clean Label No Chemicals or Additives
Bulk Supply Available OEMODM Custom Packaging
GOLD Member
Mar-26-24

Garde Ammonium Bicarbonate Cas 1066-33-7

$200 - $250
MOQ: 1  Metric Tonnes
Sample Available
 Inquire Now  
CAS:1066-33-7
Synonysm:acidammoniumcarbonate;AmmoniumBicarbonate(99.5%min) ,Ammoniumacidcarbonate,Ammoniumhydrogencarbonate;AMMONIUMBICARBONATEPChemicalbookWD;AMMONIUMBICARBONATE,REAGENTAMMONIUMBICARBONATE,REAGENTAMMONIUMBICARBONATE,REAGENT;foodgradeAmmoniumbicarbonateforbakedgoods;ammoniumbicarbonat;Ammoniumbicarbonate,99.995%metalsbasis
EINECS:213-911-5
Brand Name:Unilong
Place of Origin:Shandong, China
Purity:99%
Product name:Ammonium bicarbonate
Packing:25kgs/drum
Delivery:Immediately
MF:CH5NO3
MW:79.06

Application

1.Ammonium Bicarbonate (Food Grade) is mainly used as food expansion agent, foaming agent, neutral fertilizer, etc.
2.Ammonium Bicarbonate (Industrial Grade) can be used in pigment, leather, foam rubber, pharmacy, daily chemical industry,electroplating, ceramics, fire extinguishing agent and frosted bulb.
GOLD Member
VERIFIED
Jun-02-26
 Inquire Now  
Linear Alkyl Benzene Sulfonic Acid (LABSA) (CAS No. 68584-22-5) is a viscous brown liquid widely used as a key anionic surfactant intermediate in the detergent and cleaning industry. It is primarily utilized in the production of household and industrial detergents, liquid soaps, dishwashing liquids, laundry powders, and emulsifiers. LABSA is valued for its excellent detergency, strong emulsifying properties, and ability to remove dirt, grease, and oil effectively. It is also used in textile auxiliaries, industrial cleaners, and various formulation products requiring high foaming and cleaning performance. Known for its cost-effectiveness and strong surfactant activity, Linear Alkyl Benzene Sulfonic Acid is one of the most important raw materials in the global cleaning and detergent manufacturing industry.
GOLD Member
Nov-10-25

Super Lube Metal Protectant/corrosion Inhibitor, A

$80 - $120 / Carton (CIF)
MOQ: 500  Cartons
Supplier From North York, Ontario, Canada
 Inquire Now  
Super Lube Metal Protectant and Corrosion Inhibitor is a synthetic, penetrating oil that provides long term corrosion protection. It is designed to create a moisture displacing barrier that protects against rust and corrosion on steel, aluminum and other metal surfaces.

Super Lube Metal Protectant and Corrosion Inhibitor penetrates hard-to-reach areas while leaving a protective film to help prevent future rusting or corrosion.

Apply Super Lube Metal Protectant and Corrosion Inhibitor before storing or shipping equipment to preserve and protect from heat and humidity during adverse conditions.

Super Lube Metal Protectant and Corrosion Inhibitor is an NSF registered Food Grade lubricant, rated H1 for incidental food contact. Meets former USDA (H1) guidelines.
966685 Food Chemicals Suppliers
Short on time? Let Food Chemicals sellers contact you.
GOLD Member
Oct-14-24

Sodium Lauryl Ether Sulfate 60% (Sles)

$1.20K
MOQ: 27  Metric Tonnes
Supplier From North York, Ontario, Canada
 Inquire Now  
Sodium lauryl Ether Sulfate 60% also known as SLES 60% is a concentrated Surface-Active substance for production of liquid shampoos, dishwashing formulations, bubble baths, and hand washing agents.
Sales Specifications (Typical Results)

Active Matter: 60.1%
pH (3% Solution): 7.7
Color (5% Solution) Klett Units: 11
Ethanol: 17%
Na2SO4: 0.5
NaCl: 0.25
Unsulphonated Matter: 1.5
m.w: 427
Packing

485 lb/drum, 4 drums per pallet
2205 lb tote
DOT Transportation

UN/NA: 1170
Proper Shipping Name: Ethanol Solution
Hazard Class: 3
Packing Group: III
GOLD Member
Oct-14-24

Sodium Lauryl Ether Sulfate 70% (Sles)

$1.20K
MOQ: 27  Metric Tonnes
Supplier From North York, Ontario, Canada
 Inquire Now  
Sodium Lauryl Ether Sulfate 70 % also known as SLES 70% is a concentrated Surface-Active substance for production of liquid shampoos, dishwashing formulations, bubble baths, and hand washing agents. SLES 70 is mainly used as an emulsifier, surfactant and raw material in shampoo, bubble bath, detergent and many other personal care, cleaning and cosmetics products.
Sales Specifications

Appearance: White or light yellow gel cream
Assay: 70 ± 2
Unsulfated Matter Content: 3.0 % Max
Inorganic Sulfate Content: 2.0 % Max
Color and Luster (5% A.M. Hazen): 20 % Max
PH Value (1% AQ Solution): 7.0 % â?? 9.5 %
Dioxane (PPM): 20 PPM Max
Packing

485.012 lb drum, 4 drums per pallet
GOLD Member
Oct-12-24

Soda Ash (Ph Plus)

$800
MOQ: 27  Metric Tonnes
Supplier From North York, Ontario, Canada
 Inquire Now  
Sodium carbonate
Soda ash(PH Plus) powder
Various plastic drums, such as 50kgs, 45kgs, 40kgs, 30kgs, 25kgs, 20kgs, 15kgs, 10kgs, 5kgs, 2kgs, 1kg, 0.5kg, etc.
25kgs bags, or 1000kgs bags with pallet.
Prompt shipment within 3 weeks from confirm the order.

Packaging can be made in accordance with your requirements.
GOLD Member
Oct-12-24

Calcium Hypochlorite Granules

$1.20K
MOQ: 27  Metric Tonnes
Supplier From North York, Ontario, Canada
 Inquire Now  
Calcium hypochlorite

Effective chlorine 65% min or 70% min.
Granules.
Oval pellets(7g,10g,etc)
Tablets(10g,20g,200g,etc)
300g sticks
Prompt shipment within 3 weeks from order confirmation.

Specifications and Packaging can be made according to your requirements.
GOLD Member
Oct-12-24

Calcium Carbonate Usp/fcc

$800
MOQ: 27  Metric Tonnes
Supplier From North York, Ontario, Canada
 Inquire Now  
Sales Specification

Appearance: white powder
Identification A.B.: Pass the test
Content as CaCO3: >98.5%
Acid insolubles: 0.2%
Arsenic (As): 0.0003%
Heavy metals (as Pb): 0.0020%
Cadmium: 0.0001%
Mercury:0.00001%
Lead (as Pb): 0.3 ppm
Moisture: 2%
Magnesium & Alkali Salts: 1%
Barium: Negative
Iron: 0.02%
Fluoride: 0.005%
Chlorides: 0.033%
Sulphate: 0.2%
OVI: Pass the test
Bulk density: 1.0 to 1.2g/ml
Packing

55.12 lb bag, 40 bags per pallet
GOLD Member
Oct-12-24

Hydrogen Peroxide 50%

$800
MOQ: 27  Metric Tonnes
Supplier From North York, Ontario, Canada
 Inquire Now  
Hydrogen Peroxide 50% is used as an oxidizer, bleaching agent ,cleaning agent, antiseptic . Hydrogen peroxide has various industrial uses, primarily as a cleaning agent. It is used as a cleaning agent in homes and hospitals, to bleach hair, to bleach paper and textile products, detoxification of industrial waste, in wastewater treatment, in detergent, in the manufacturing of food products, process minerals and petrochemicals, horticulture, fish keeping and in photography.
Specifications

Appearance Clear,Colorless Liquid
Concentration ±0.5
Density 1.1925
Acidity Max 0.06
Stability Max 0.3
Iron Content Max 0.03
pH 1.01
Packing

551.15 Lb Drum, 4 Drums per pallet
DOT Transportation

UN/NA: 2014
Proper Shipping Name: Hydrogen peroxide, aqueous solution
Class: 5.1 (8)
Packing Group: II
GOLD Member
VERIFIED
Jun-01-26

E-Bei 1.0 Enzyme For Ethanol Production, Industrial Grade

$0.12 - $0.12 / Kilogram (FOB)
MOQ: Not Specified
Supplier From Bogor, Jawa Barat, Indonesia
 Inquire Now  
e-BE1.0 is a high-performance enzyme consortium specifically developed to enhance ethanol production efficiency from molasses-based fermentation processes. The product helps convert unfermentable sugars into fermentable sugars, enabling higher ethanol yields and improved production performance.

Designed for industrial ethanol manufacturers, e-BE1.0 supports more efficient sugar utilization during fermentation by increasing the availability of fermentable sugars in raw materials. This enzymatic action contributes to improved productivity, optimized fermentation efficiency, and better overall process economics.

The liquid enzyme formulation is easy to apply and can be added directly to the raw material dilution tank before fermentation. Suitable for molasses-based ethanol production systems, e-BE1.0 offers reliable performance and consistent results under various processing conditions.

Product Highlights
- Specialized enzyme consortium for ethanol production
- Converts unfermentable sugars into fermentable sugars
- Helps increase ethanol yield
- Supports efficient fermentation processes
- Suitable for molasses-based ethanol production
- Easy-to-apply liquid formulation
- Reliable industrial performance
- Consistent production efficiency improvement

Applications
- Ethanol production plants
- Molasses fermentation processes
- Bioethanol manufacturing
- Industrial fermentation systems
- Sugar conversion enhancement
- Yield improvement programs

Technical Specifications
- Appearance: Dark brown liquid
- Density: 1.000 -1.200 g/ml
- pH Range: 3.0 - 7.0
- Solubility: Soluble in water

Packaging
Available in:
- 30 kg plastic jerry can
- 200 kg plastic drum

Storage
Store in cool and dry conditions away from direct sunlight and rain. Shelf life is up to 6 months at 25C and up to 1 year at 10C.

e-BE1.0 is an effective industrial enzyme solution for ethanol producers seeking higher fermentation efficiency, improved sugar conversion, and increased ethanol production yields.
GOLD Member
VERIFIED
Jun-01-26

Sb-Ds05 Deinking Enzyme For Paper Industry, Industrial Grade

$0.12 - $0.12 / Kilogram (FOB)
MOQ: Not Specified
Supplier From Bogor, Jawa Barat, Indonesia
 Inquire Now  
SB-DS05 is a high-performance liquid deinking enzyme specially developed for recycled paper processing and pulp manufacturing applications. The product effectively removes color spots and ink contaminants, including water-soluble inks from washing processes and toner inks generated during flotation systems.

SB-DS05 is designed to improve color contaminant removal efficiency while significantly enhancing pulp brightness, especially when processing low-quality recovered paper. The enzyme-based formulation helps paper manufacturers achieve cleaner pulp, improved paper quality, and more efficient production performance.

Compared to conventional chemical treatments, SB-DS05 provides an environmentally friendly solution that is safer to use and will not damage plant equipment or mechanical systems. The product also contributes to improved papermachine runnability and supports more sustainable paper manufacturing operations.

Product Highlights
- High-performance liquid deinking enzyme
- Improves pulp brightness
- Reduces residual color specks by up to 40%
- Supports recycled paper processing
- Environmentally friendly formulation
- Safe for plant equipment and mechanical systems
- Enhances papermachine runnability
- Suitable for low-quality recovered paper applications

Applications
- Recycled paper processing
- Pulp and paper manufacturing
- Deinking flotation systems
- Waste paper recycling plants
- Paper brightness improvement processes
- Color contaminant removal applications

Technical Specifications
- Appearance: Yellowish to brownish liquid
- Form: Liquid enzyme
- Application: Deinking and pulp brightness improvement
- Packaging: 30 kg jerry can or 200 kg plastic drum

Storage
Store in cool and dry conditions away from direct sunlight and rain. Recommended shelf life is 6 months at 20C.

SB-DS05 is an effective industrial enzyme solution for paper manufacturers seeking improved pulp quality, better contaminant removal, and environmentally responsible production processes.
GOLD Member
VERIFIED
Jun-02-26

Sb-Sc25 Stickies Control Enzyme For Paper, Industrial Grade

$0.12 - $0.12 / Kilogram (FOB)
MOQ: Not Specified
Supplier From Bogor, Jawa Barat, Indonesia
 Inquire Now  
SB-SC25 is a high-performance enzyme solution specifically developed to control sticky contaminants in paper manufacturing processes. The product effectively attacks and reduces sticky materials commonly found in recycled fiber and paper production systems, helping improve machine efficiency and operational reliability.

By minimizing sticky deposits, SB-SC25 helps reduce paper machine breaks, decrease downtime, and improve overall production efficiency. The enzyme also contributes to cleaner paper sheets by eliminating sticky contaminants that can negatively affect product quality and machine performance.

As an environmentally responsible alternative, SB-SC25 helps reduce the need for harsh chemical solvents traditionally used for cleaning and deposit control. This supports safer and more sustainable paper manufacturing operations while maintaining consistent process performance.

Product Highlights
- Specialized enzyme for stickies control
- Reduces sticky material deposits
- Helps prevent paper machine breaks
- Improves operational efficiency
- Reduces machine downtime
- Supports cleaner paper production
- Helps reduce harsh chemical usage
- Suitable for paper manufacturing processes

Applications
- Paper manufacturing
- Recycled paper processing
- Pulp and paper mills
- Deposit control programs
- Stickies management systems
- Paper machine performance improvement

Packaging available in:
- 30 kg plastic jerry can
- 200 kg plastic drum

Storage
Store in cool and dry conditions away from direct sunlight and rain. Shelf life is up to 6 months at 20C under recommended storage conditions.

SB-SC25 is an effective enzyme solution for paper manufacturers seeking improved machine performance, reduced downtime, enhanced product quality, and efficient stickies control.
GOLD Member
VERIFIED
Jun-02-26

E-Wash 1.0 Multi-Enzyme For Detergents, Industrial Grade

$0.12 - $0.12 / Kilogram (FOB)
MOQ: Not Specified
Supplier From Bogor, Jawa Barat, Indonesia
 Inquire Now  
e-Wash 1.0 is a high-performance multi-enzyme solution specially developed for liquid detergent formulations and industrial laundry applications. This advanced enzyme blend combines protease, lipase, amylase, cellulase, and papain to deliver comprehensive stain removal and enhanced washing performance across a wide range of fabric care applications.

Designed for detergent manufacturers, e-Wash 1.0 effectively removes protein, fat, grease, starch, and particulate dirt stains while helping maintain fabric softness and garment quality. The synergistic interaction between enzymes and surfactants provides superior cleaning efficiency and supports reduced surfactant usage, helping optimize detergent formulation costs.

The product operates efficiently across a broad temperature and pH range, making it suitable for various detergent manufacturing processes. Its biodegradable formulation supports environmentally responsible cleaning solutions while delivering reliable washing performance.

Product Highlights
- Advanced multi-enzyme detergent solution
- Contains protease, lipase, amylase, cellulase, and papain
- Effective against protein, starch, fat, and grease stains
- Compatible with neutral liquid detergent formulations
- High stability under normal washing conditions
- Helps reduce surfactant consumption
- Improves fabric softness and garment care
- Biodegradable and environmentally friendly

Applications
- Liquid detergent manufacturing
- Laundry detergent formulations
- Household cleaning products
- Industrial laundry processing
- Fabric care products
- Enzyme-based detergent systems

Technical Specifications
- Appearance: Brown translucent liquid
- pH: 4.0-6.0
- Solubility: Miscible with water
- Operating Temperature: 20- 70 �°C
- Operating pH: 5.0-8.0

Packaging
- Available in 30 kg plastic drums. Custom packaging options are available upon request.

Storage
- Store in cool and dry conditions away from direct sunlight and rain. Shelf life is up to 6 months at 25 �°C. Cooler storage conditions are recommended.

e-Wash 1.0 is an effective enzyme solution for detergent manufacturers seeking improved cleaning performance, enhanced stain removal, reduced formulation costs, and environmentally friendly detergent technologies.
Storage

Store in cool and dry conditions away from direct sunlight and rain. Shelf life is up to 6 months at 25C. Cooler storage conditions are recommended.

e-Wash 1.0 is an effective enzyme solution for detergent manufacturers seeking improved cleaning performance, enhanced stain removal, reduced formulation costs, and environmentally friendly detergent technologies.
GOLD Member
VERIFIED
Jun-01-26

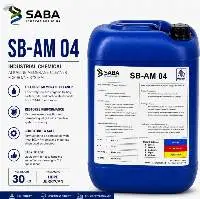
Sb Am-04 Starch Enzyme For Paper Sizing, Industrial Grade

$0.12 - $0.12 / Kilogram (FOB)
MOQ: Not Specified
Supplier From Bogor, Jawa Barat, Indonesia
 Inquire Now  
SB Am-04 is a high-performance liquid enzyme specifically developed for starch modification in paper sizing and coating applications. The product effectively hydrolyzes gelatinized starch, resulting in rapid viscosity reduction and improved starch processing performance for paper manufacturing operations.

Designed for paper mills and pulp processing facilities, SB Am-04 helps optimize starch-based formulations used in paper sizing and coating systems. Its enzymatic action improves process efficiency, supports consistent starch preparation, and enhances production performance in modern paper manufacturing environments.

As a liquid enzyme solution, SB Am-04 is easy to handle and integrate into existing production processes. It provides a reliable and environmentally friendly alternative for starch viscosity control while supporting stable paper production quality.

Product Highlights
- High-performance liquid starch enzyme
- Designed for paper sizing applications
- Suitable for paper coating formulations
- Rapid viscosity reduction capability
- Efficient starch hydrolysis performance
- Easy application in industrial processes
- Reliable quality and stable performance
- Suitable for paper manufacturing operations

Applications
- Paper sizing processes
- Paper coating formulations
- Starch modification
- Paper manufacturing
- Pulp and paper industry
- Industrial starch processing

Packaging
Available in 30 kg plastic jerry can.

Storage
Store in cool and dry conditions away from direct sunlight and rain. Recommended shelf life is up to 6 months at 20C.

SB Am-04 is an effective enzyme solution for paper manufacturers seeking efficient starch hydrolysis, viscosity control, and improved paper sizing performance.
GOLD Member
VERIFIED
May-26-26

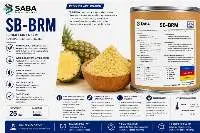
Sb - Brm, High Performance Industrial Grade Bromlain Enzyme

$0.12 - $0.12 / Kilogram (FOB)
MOQ: Not Specified
Supplier From Bogor, Jawa Barat, Indonesia
 Inquire Now  
SB-BRM is a premium industrial bromelain enzyme extracted from natural pineapple stem and pericarp. This high-performance protease enzyme is specially developed for efficient protein hydrolysis and industrial enzymatic processing across various industries. SB-BRM offers stable activity, reliable quality, and excellent processing performance for modern manufacturing applications.

Widely used in food processing, pharmaceuticals, cosmetics, and feed industries, SB-BRM helps improve product quality, optimize protein breakdown, and support efficient industrial production processes. Its strong proteolytic activity makes it suitable for multiple industrial applications requiring effective enzymatic performance.

Product Highlights
- Premium industrial bromelain enzyme
- Natural pineapple extract enzyme
- Strong protein hydrolysis capability
- High enzymatic activity up to 2400 GDU/g
- Water-soluble and easy to apply
- Stable processing performance
- Suitable for large-scale industrial applications
- Consistent export-quality standard

Main Applications
- Meat tenderizing
- Dough softening and bakery processing
- Cheese processing
- Protein and beverage production
- Pharmaceutical formulations
- Cosmetics and skincare products
- Feed additives and protein utilization improvement

Technical Specifications
- Appearance: Light yellow powder
- Solubility: Soluble in water
- Optimum Temperature: 30-45 C
- Optimum pH: 6.0-8.0
- Activity: 2400 GDU/g

Packaging
Available in 5 kg, 20 kg, and 25 kg.

Storage
Store in a cool and dry place away from direct sunlight, heat, and moisture. Shelf life is up to 24 months under recommended storage conditions.

SB-BRM is a reliable industrial enzyme solution for manufacturers seeking stable quality, efficient enzymatic performance, and professional-grade industrial processing support.
GOLD Member
VERIFIED
May-26-26

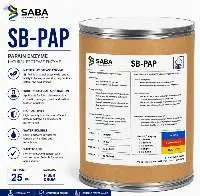
Sb - Pap, Food Grade

$0.12 - $0.12 / Kilogram (FOB)
MOQ: Not Specified
Supplier From Bogor, Jawa Barat, Indonesia
 Inquire Now  
SB-PAP is a premium industrial papain enzyme designed for efficient protein hydrolysis and high-performance enzymatic processing across multiple industries. Produced from natural papaya extract, SB-PAP provides strong proteolytic activity, stable performance, and reliable quality for industrial manufacturing applications.

This industrial enzyme is widely used in the food, pharmaceutical, cosmetic, detergent, feed, leather, and textile industries. SB-PAP helps improve processing efficiency, optimize protein breakdown, enhance product quality, and support cost-effective production operations.

Product Highlights
- Premium industrial papain enzyme
- High enzymatic activity up to 100,000 U/g
- Strong protein hydrolysis capability
- Water-soluble and easy to apply
- Stable processing performance
- Suitable for large-scale industrial applications
- Consistent export-quality standard

Main Applications
- Meat tenderizing
- Beer clarification
- Bakery & biscuit processing
- Pharmaceutical formulations
- Cosmetics & skincare products
- Detergent & cleaning products
- Animal feed additives
- Leather & textile processing

Technical Specifications
- Appearance: White powder
- Solubility: Soluble in water
- Optimum Temperature: 50-55 �°C
- Optimum pH: 6.0-7.0
- Reaction Time: 6-8 hours
- Activity: 100,000 U/g

Packaging
Available 5 kg, 20 kg, and 25 kg.

Storage
Store in a cool and dry place away from direct sunlight, heat, and moisture. Shelf life is up to 12 months in unopened packaging.

SB-PAP is a reliable industrial enzyme solution for manufacturers seeking high-efficiency, stable quality, and professional-grade performance for modern industrial processing.
GOLD Member
VERIFIED
Jun-01-26

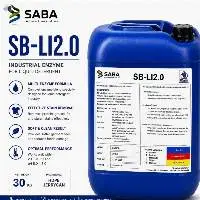
Sb-Li2.0 Liquid Lipase Enzyme, Industrial Grade

$0.12 - $0.21 / Kilogram (FOB)
MOQ: Not Specified
Supplier From Bogor, Jawa Barat, Indonesia
 Inquire Now  
SB-LI2.0 is a high-performance liquid lipase enzyme produced through submerged fermentation of selected high lipase-producing microbial strains. The enzyme is specifically designed to hydrolyze fats and oils by breaking down mono-, di-, and triglycerides into glycerol and fatty acids, providing efficient lipid degradation for industrial applications.

With strong enzymatic activity of 10,000 U/mL, SB-LI2.0 delivers reliable performance across a broad operating pH range, making it suitable for various industrial formulations. The enzyme is particularly effective in detergent applications, helping improve the removal of grease, oil, and fat-based stains while enhancing overall cleaning efficiency.

Its liquid formulation allows easy handling and integration into manufacturing processes. SB-LI2.0 offers stable activity, consistent quality, and dependable performance for industrial users seeking advanced enzymatic solutions for fat degradation and cleaning applications.

Product Highlights
- High-performance liquid lipase enzyme
- Activity up to 10,000 U/mL
- Efficient fat and oil degradation
- Broad operating pH range
- Water-soluble liquid formulation
- Suitable for detergent applications
- Stable and reliable enzymatic performance
- Consistent industrial-grade quality

Applications
- Detergent manufacturing
- Industrial cleaning products
- Fat and oil degradation processes
- Enzyme-based cleaning formulations
- Industrial biochemical processing
- Specialty chemical applications

Technical Specifications
- Appearance: Amber to brown liquid
- Activity: 10,000 U/mL
- Density: 1.000 - 1.200 g/mL
- Operating pH: 4.0 - 10.0
- Optimum pH: 6.5 - 7.5
- Solubility: Soluble in water

Packaging
Available in 30 kg plastic jerry can.

Storage
Store in cool and dry conditions away from direct sunlight and rain. Shelf life is up to 6 months at 25C under recommended storage conditions.

SB-LI2.0 is an effective industrial enzyme solution for manufacturers seeking enhanced fat degradation, improved cleaning performance, and reliable enzymatic processing efficiency.
GOLD Member
VERIFIED
Jun-01-26

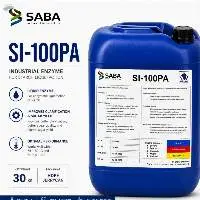
Si 100 Pa Starch Liquefaction Enzyme, Industrial Grade

$0.10 - $0.50 / Kilogram (FOB)
MOQ: Not Specified
Supplier From Bogor, Jawa Barat, Indonesia
 Inquire Now  
SI 100 PA is a high-performance liquid enzyme specifically developed for starch liquefaction and sugar processing applications. The enzyme hydrolyzes 1,4 glycosidic bonds in amylose and amylopectin, converting starch into soluble oligosaccharides to improve process efficiency and product quality.

Designed for the sugar industry, SI 100 PA helps enhance clarification performance, improve sugar quality, and increase sugar yield during production. Its enzymatic action supports more efficient starch conversion while contributing to improved operational performance in sugar processing facilities.

The liquid formulation is easy to apply and can be added directly into melter tanks. SI 100 PA performs effectively across a broad temperature and pH range, providing reliable results under various processing conditions.

Product Highlights
- High-performance starch liquefaction enzyme
- Converts starch into soluble oligosaccharides
- Improves sugar clarification
- Enhances sugar quality and yield
- Easy-to-apply liquid formulation
- Water-soluble enzyme preparation
- Reliable industrial performance
- Suitable for sugar processing operations

Applications
- Sugar manufacturing
- Sugar refining
- Starch liquefaction processes
- Raw sugar processing
- Sugar clarification improvement
- Industrial carbohydrate processing

Technical Specifications
- Appearance: Dark brown liquid
- Density: 1.000-1.200 g/ml
- pH Enzyme: 4.0-7.0
- Working Temperature: 65-80C
- Working pH: 5.5-8.5
- Solubility: Soluble in water

Packaging
Available in 30 kg plastic jerry can.

Storage
Store in cool and dry conditions away from direct sunlight and rain. Shelf life is up to 6 months at 25C under recommended storage conditions.

SI 100 PA is an effective enzyme solution for sugar manufacturers seeking improved starch conversion, higher sugar yield, better clarification, and enhanced production efficiency.
966685 Food Chemicals Suppliers
Short on time? Let Food Chemicals sellers contact you.
Explore Food Chemicals related import export discussions